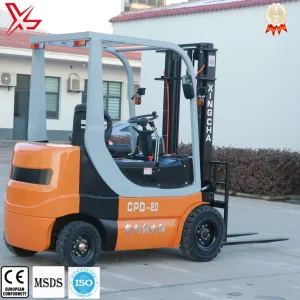
Architecting High-Efficiency Material Handling Systems: Modular Engineering, Advanced Electrification, ATEX Safety, and Global OEM/ODM Infrastructure
Explore our top-tier heavy equipment, electric forklifts, telescopic handlers, and custom material handling solutions designed for demanding industrial operations.
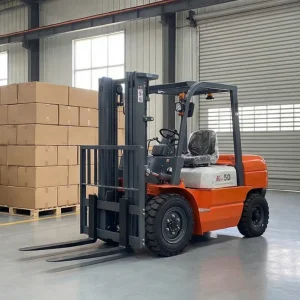


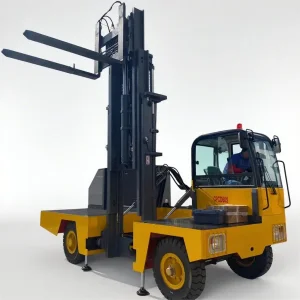

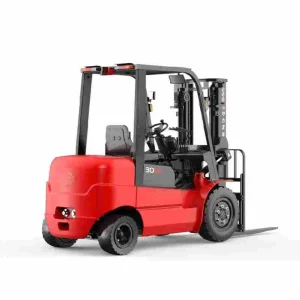
Transitioning from standard mass-manufactured material handling equipment to high-performance, tailored engineering frameworks optimized for TCO and operational specifics.
In modern logistics, warehousing, mining, and chemical manufacturing, off-the-shelf material handling machinery frequently falls short of meeting complex spatial, environmental, and duty-cycle constraints. Enterprise buyers no longer demand generic lifting capacity; they require custom-architected machinery built around exact load dynamics, operating temperatures, and site-specific floor gradients.
Custom OEM (Original Equipment Manufacturer) forklift solutions bridge the critical gap between standardized specs and site realities. By modifying structural dimensions, integrating specialized attachments, configuring explosion-proof (ATEX) drive motors, and optimizing powertrain electronics, specialized manufacturers deliver machinery that dramatically amplifies throughput while mitigating structural stress and operator fatigue.
Next-generation technological convergence: Electrification, IoT telematics, autonomous readiness, and ergonomic human-machine interfaces.
The rapid transition from traditional lead-acid batteries and heavy internal combustion to high-density Lithium Iron Phosphate (LiFePO4) chemistry represents a watershed moment. Modern OEM electric forklifts offer opportunity charging (full charge in 1-2 hours), zero toxic off-gassing, 4,000+ lifecycle charges, and a 30% reduction in thermal loss, making all-electric and hybrid power the global benchmark for warehouse compliance.
Modern OEM forklifts feature controller area network (CAN-bus) architectures paired with cloud telematics modules. Real-time data streams monitor motor heat, hydraulic pressure, battery State of Health (SOH), operator driving telemetry, and impact detection. Predictive maintenance algorithms drastically eliminate unscheduled downtime across global logistics fleets.
For chemical processing plants, oil refineries, and pharmaceutical manufacturing, custom OEM solutions deliver certified explosion-proof (EX) configurations. Enclosed AC motors, intrinsically safe switches, conductive tires, and temperature-monitored brake systems prevent electrical arching and surface heating capable of igniting airborne dust or volatile chemical vapors.
Why international procurement directors partner with specialized China-based source factories for custom forklift and construction equipment production.
China's material handling and construction machinery ecosystem—centered heavily in industrial manufacturing clusters like Anhui Province—offers unprecedented structural advantages in vertical integration, speed-to-market, and custom engineering flexibility.
Unlike traditional Western OEMs bounded by rigid assembly line standardization, Chinese specialized source factories excel in modular, low-to-medium volume OEM/ODM customizations. Enterprise clients can specify custom chassis widths, specialized mast lift heights (3m to 7m+), customized hydraulic valve blocks, and brand-specific aesthetic branding without incurring prohibitive tooling costs.
Located in Hefei, Anhui Province—the core manufacturing heartland for leading industrial machinery—companies benefit from immediate proximity to world-class hydraulic pump foundries, high-tensile steel rolling mills, and battery cell gigafactories. This geographical proximity cuts component sourcing lead times by up to 60%.
| Evaluation Metric | Standard Global OEMs | China Custom Source Factory |
|---|---|---|
| Customization Scope | Restricted to static option catalogs | Full engineering adaptation (Chassis, Hydraulics, EX) |
| OEM Lead Time | 24 - 36 Weeks | 6 - 12 Weeks |
| CapEx Investment | High Premium (Brand Overhead) | Optimized Factory Direct Costing |
| Spare Part Availability | Proprietary Lock-in | Standardized / Interchangeable Global Components |
| Modular Agility | Low flexibility for short runs | High capacity for specialized batch production |
Tailoring heavy machinery and forklift engineering to the rigorous operational demands of key global industries.
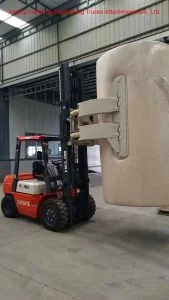
Paper rolls and raw cellulose reels require delicate yet high-pressure handling to prevent outer layer damage. Custom forklifts equipped with hydraulic 360-degree rotating paper roll clamps allow smooth horizontal-to-vertical positioning during mill unloading and high-density warehouse stacking.
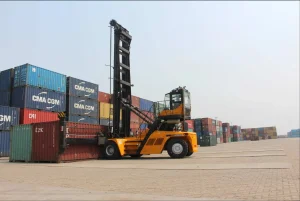
Intermodal terminals and container freight stations require heavy-duty handling equipment capable of stacking empty ISO containers up to 7-8 tiers high. Specialized Heavy Duty Empty Container Handlers (9T-10T capacity) provide maximum stability under high wind loads.
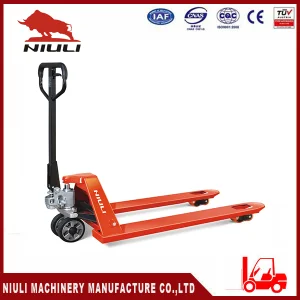
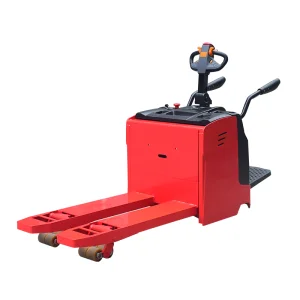
Volatile solvent handling and explosive powder environments present severe ignition risks. Specialized explosion-proof electric pallet trucks and counterbalanced forklifts utilize fully sealed AC brushless drive motors and anti-static poly wheels.
Unpaved mud, gravel yards, and agricultural orchards require machinery with high ground clearance, deep-tread tires, and robust torque output. Mini Rough Terrain Telescopic Handlers combine forklift lifting capabilities with crane reach versatility.
Sub-zero cold storage facilities (-30°C) cause severe condensation, battery capacity drop, and hydraulic fluid thickening. OEM cold-store customization ensures seamless, non-stop warehouse throughput.
As industrial real estate costs escalate, logistics centers transition to narrow aisle layouts. Compact electric pallet stackers and counterbalanced reach trucks maximize vertical cubic storage space.
Hefei GLS Forklift Co., Ltd. is a specialized manufacturer and exporter of high-performance construction machinery, headquartered in Anhui province, China. GLS machinery products include: excavators, loaders, road rollers, forklifts, and small tracked vehicles. With over a decade of R&D and production expertise, we have established ourselves as a trusted partner in the construction equipment and material handling industry.
Over a decade of production and sales experience; quality assured directly from the manufacturing floor.
Actively incorporates advanced robotic welding and intelligent testing processes to boost durability.
Exported to Asia, South America, Africa, Europe, and the Middle East across 100+ countries and regions.
Every machine leaving the Hefei GLS manufacturing facility undergoes multi-stage load testing, tilt-stability verification, and hydraulic pressure decay audits.
Meets all European health, safety, and environmental protection requirements.
Standardized manufacturing workflows ensuring batch-to-batch product consistency.
Rapid adaptation to mining, forestry, agriculture, and urban construction scenarios.
Evaluating CapEx versus OpEx in high-duty material handling machinery investments.
Direct factory sourcing eliminates distributor markups, allowing procurement teams to allocate capital toward functional enhancements such as LiFePO4 battery upgrades or specialized hydraulic clamps that directly boost daily pallet throughput.
Machine downtime is the single largest cost driver in warehouse operations. Partnering with suppliers offering genuine replacement parts (e.g., replacement water pipes, hydraulic seal kits, AC controllers) ensures rapid maintenance cycles and minimal operational disruption.
Switching diesel fleets to high-efficiency electric or LPG/Gasoline hybrid drivetrains cuts fuel overhead by up to 65% per operational shift while satisfying stringent corporate ESG (Environmental, Social, and Governance) targets.
Expert answers to common OEM customization, shipping, certification, and engineering inquiries.
Browse additional high-performance pallet trucks, rough terrain telescopic handlers, specialized attachments, and heavy container machinery.


 GLS Forklift